

How to Choose a Battery Shuttle Car for Your Stone Factory?
A battery shuttle car is a self-powered, remote-controlled transport vehicle used in Stone Fabrication facilities to move granite slabs, marble blocks, and engineered stone panels between processing stations without fixed rails or trailing cables. Choosing the right model requires evaluating five interdependent factors: load capacity, battery endurance, table dimensions, floor conditions, and control system compatibility. This guide provides a structured decision framework based on real production parameters, helping factory managers match equipment specifications to operational requirements without over-engineering the investment.
Key takeaways: 1) Evaluate actual maximum slab weight, not average weight, when sizing load capacity. 2) Battery runtime must cover one full shift without mid-day charging — 8+ hours is the baseline. 3) Table size must accommodate the largest slab dimension processed, including overhang allowance. 4) Wheel diameter selection depends on floor surface quality — 400–630 mm wheels suit standard concrete floors.
What Does a Battery Shuttle Car Do in a Stone Factory
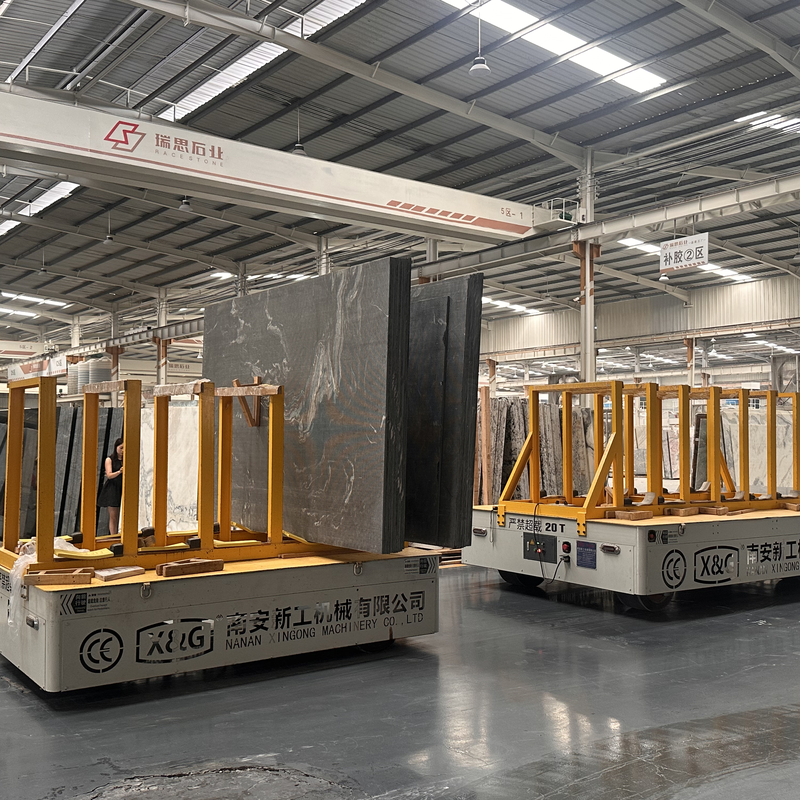
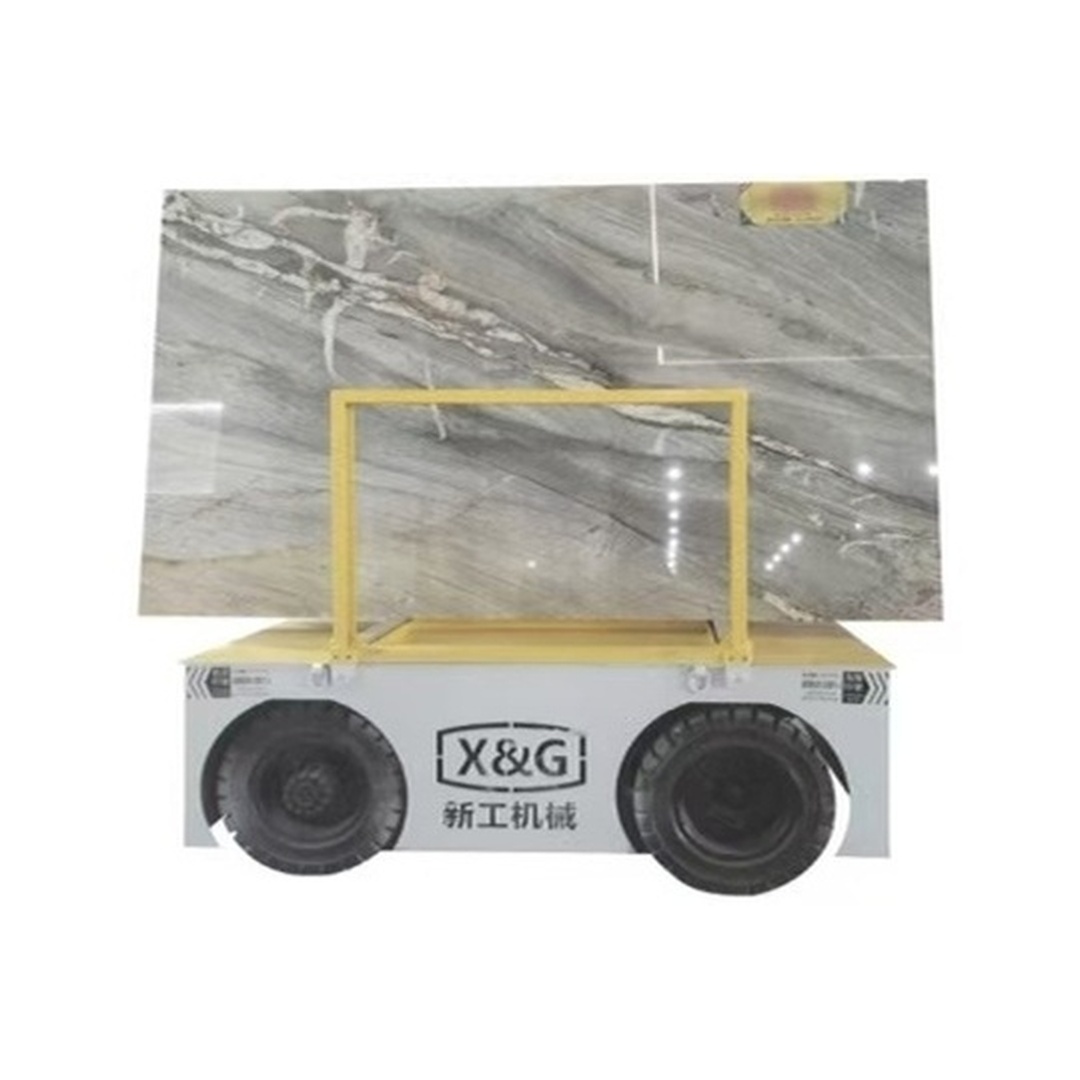
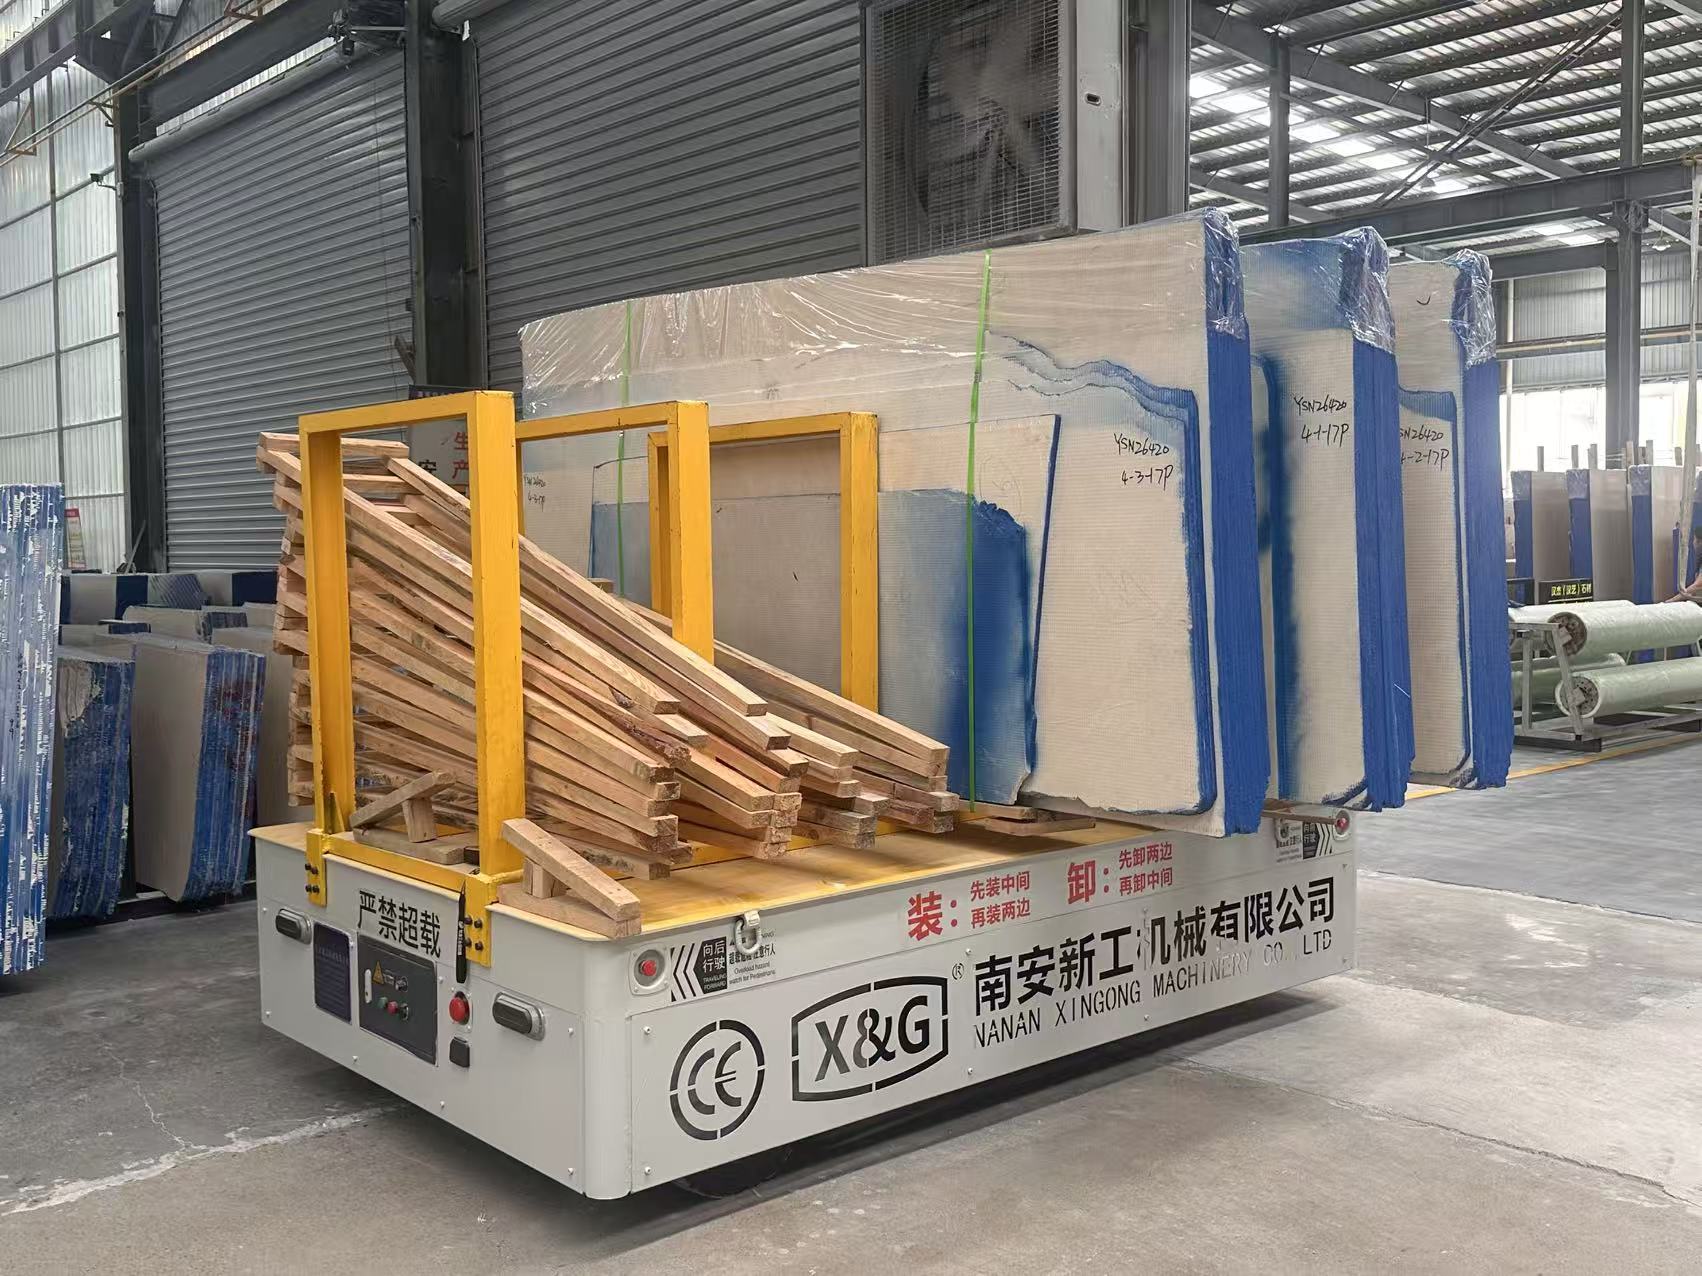
A battery shuttle cartransports heavy stone materials from one workstation to another — for example, from slab storage racks to a Bridge Saw, or from a saw to a polishing line. Unlike fixed rail carts that run on embedded tracks, a battery shuttle car moves freely across the factory floor, guided by a wireless remote control. This freedom of movement is its main advantage: layout changes do not require track relocation, and multiple carts can share the same workspace without physical track conflicts.
The vehicle consists of a battery power source, an electric traction motor, a steel load platform, and a control module with obstacle detection. When the operator sends a command via remote, the cart moves forward, backward, or rotates in place — typical trackless models achieve 60-degree in-situ rotation. According to OSHA material handling guidelines, removing fixed obstacles such as rails from factory floors reduces trip hazards and improves workspace flexibility, which is one reason battery shuttle cars are increasingly specified in new stone fabrication plants.
Step 1: Determine the Required Load Capacity
The most critical parameter when you choose a battery shuttle car for your stone factory is load capacity. Under-rating this value leads to frequent overload shutdowns and accelerated motor wear. Over-rating it adds unnecessary cost. The correct approach is to identify the heaviest single slab or block that will be transported on a regular basis, then apply a 1.25× safety margin.
A typical granite slab measuring 3,000 × 2,000 × 30 mm weighs approximately 450 kg. A single-slab pallet of four stacked slabs reaches roughly 1,800 kg. A stone block for monument fabrication can exceed 8,000 kg. Most stone fabrication facilities fall within two standard capacity tiers:
| Capacity Tier | Max Payload | Typical Applications | Recommended Model |
|---|---|---|---|
| Standard | 10,000 kg | Individual slabs, small block transport | XGM-BDC10T |
| Heavy-duty | 20,000 kg | Multi-slab pallets, large stone blocks | XGM-BDC20T |
The 10,000 kg tier covers the majority of individual slab transport needs. The 20,000 kg tier is recommended when the facility regularly moves stacked slabs or bulk stone blocks. Both tiers should be verified against the actual lifting capacity of the overhead crane or forklift used for loading, since transport capacity must match upstream handling capacity.
Step 2: Evaluate Battery Runtime and Charging Infrastructure
Battery endurance directly determines whether the shuttle car can complete a full shift without interruption. When you choose a battery shuttle car, the continuous working hours per charge must be equal to or greater than the longest production shift. Industry-standard Dv200 lead-acid battery packs on the XGM-BDC series provide more than 8 hours of continuous operation, which covers a standard single shift.
Key battery specifications to compare:
- Charge cycles: Dv200 packs are rated for over 1,000 charge cycles. At one full cycle per day, this translates to approximately 3 years of daily use before replacement.
- Charging time: The XGM-BDC10T charges in under 6 hours; the XGM-BDC20T in under 8 hours. Overnight charging between shifts is standard practice.
- Battery configuration: The 10-ton model uses 6 × Dv200 batteries; the 20-ton model uses 8 × Dv200 batteries. Higher battery count increases both capacity and replacement cost.
Facilities running double shifts should consider purchasing two battery packs per cart, allowing one pack to charge while the other is in use. The ISO 13849 safety standard for industrial vehicle control systems provides relevant guidelines for battery management system integration in powered industrial trucks.
Step 3: Match Table Dimensions to Slab Sizes
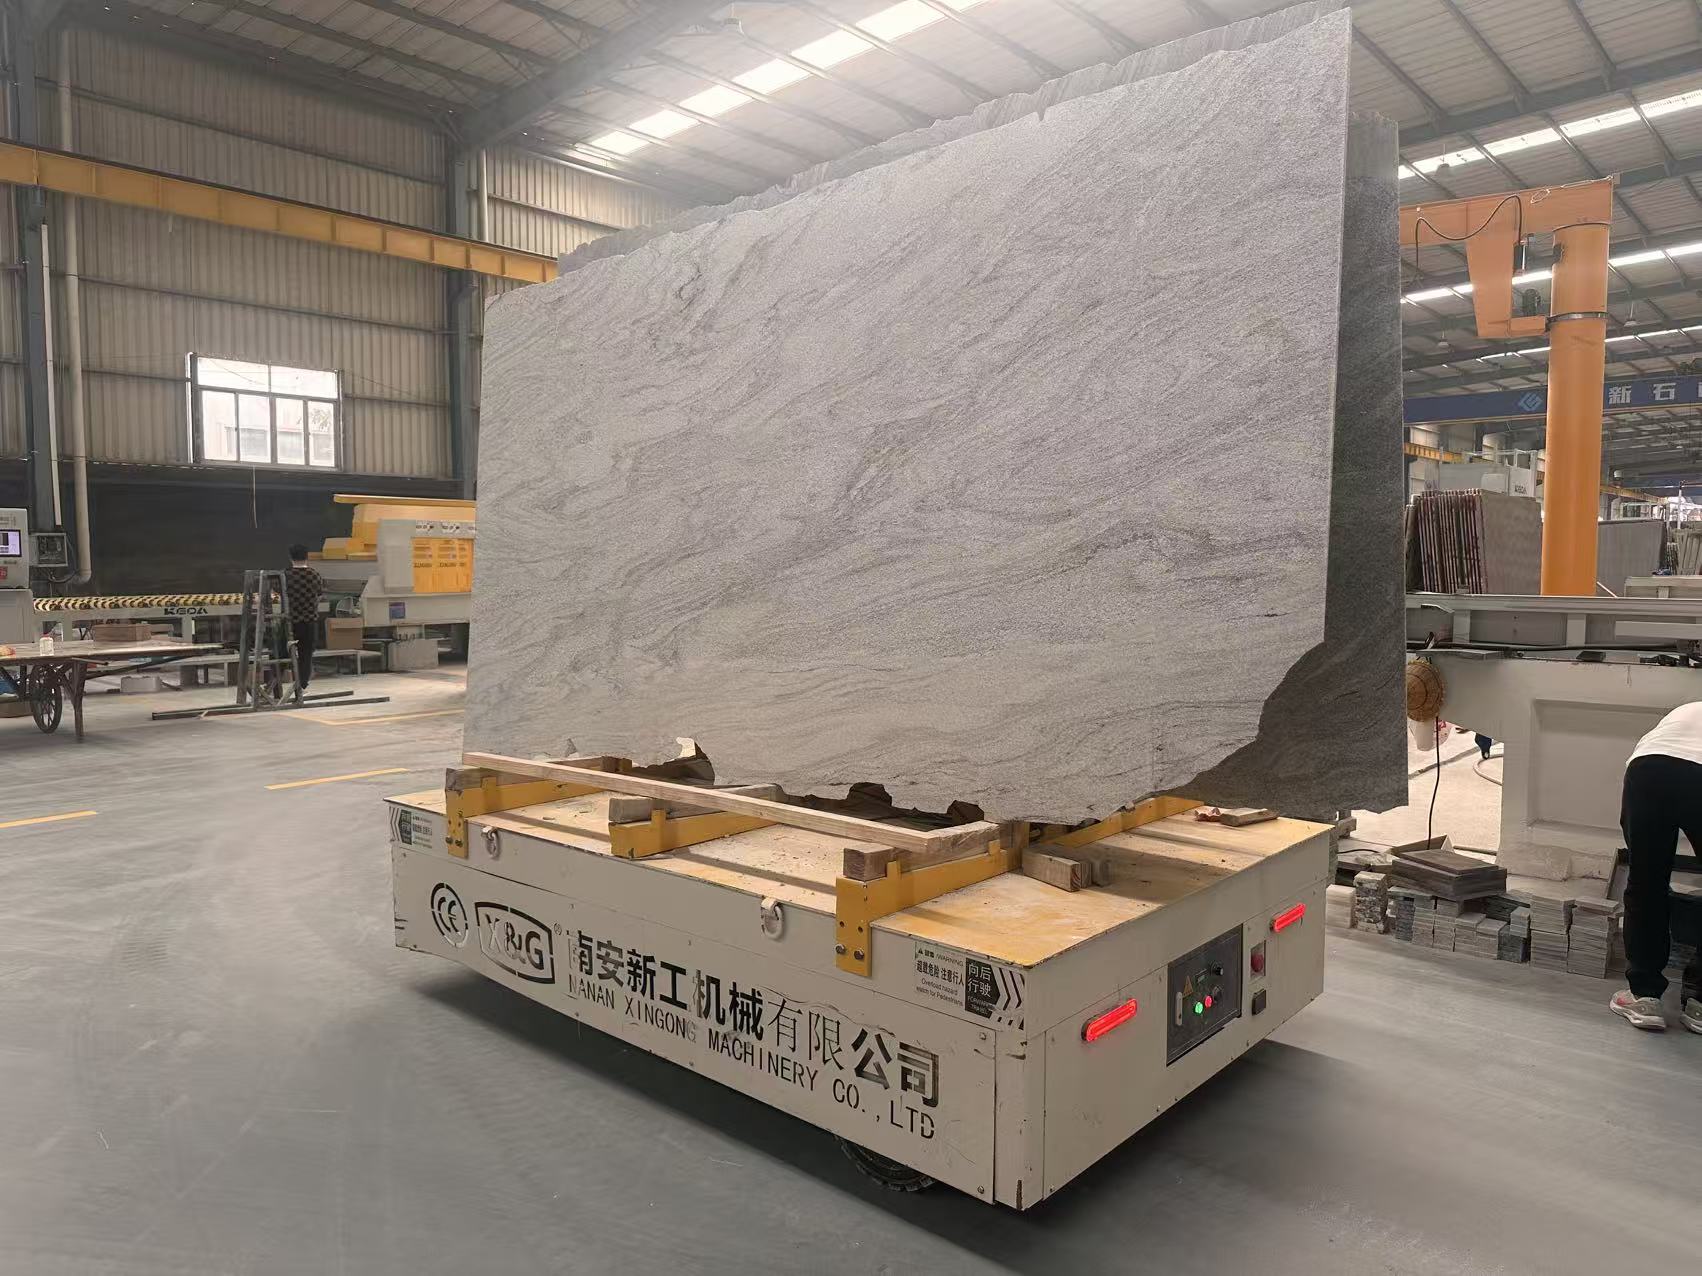
The load table of the shuttle car must be dimensioned for the largest slab the facility processes. A slab that overhangs the table edges by more than 200 mm risks instability during movement, especially when the cart travels at the standard speed of 20 m/min.
The XGM-BDC10T offers a table size of 2,500 × 2,000 mm, suitable for standard slab dimensions up to 2,400 × 1,800 mm. The XGM-BDC20T provides a 3,000 × 2,000 mm table, accommodating jumbo slabs up to 3,000 × 2,000 mm — a common size in architectural cladding production. Optional accessories such as positioning fixtures and clamping devices can be added to secure irregularly shaped loads, and these are available across the battery trackless transfer car series from Xiigoo.
Step 4: Assess Floor Conditions and Wheel Selection
Wheel diameter and material directly affect the shuttle car's stability and maintenance frequency. Larger wheels handle floor unevenness better but raise the load platform height, which may require adjustments at loading stations.
| Floor Condition | Recommended Wheel Diameter | Wheel Material | Notes |
|---|---|---|---|
| Smooth industrial concrete (±3 mm tolerance) | 400 mm | Solid steel with polyurethane tread | Low vibration, higher load rating |
| Standard concrete (±5 mm tolerance) | 400–630 mm | All-steel or reinforced polyurethane | XGM-BDC20T uses 400 mm; XGM-BDC10T uses 630 mm |
| Uneven or aged concrete floor | 630 mm or larger | All-steel with hardened rim | Larger wheels bridge gaps better |
The difference in wheel diameters between the XGM-BDC10T (630 mm) and XGM-BDC20T (400 mm) reflects their different design priorities: the 10-ton model emphasizes floor clearance, while the 20-ton model prioritizes lower platform height for easier slab loading. Factory floor surveys should be conducted before final model selection.
Step 5: Choose Between Trackless and Rail-Compatible Models
When you choose a battery shuttle car for your stone factory, a secondary decision is whether a fully trackless model or a rail-compatible model better suits the production layout. Trackless battery shuttle cars, such as those in Xiigoo's trackless series, operate on any solid floor and can change paths instantly. They achieve 60-degree in-situ rotation and include obstacle detection that automatically stops the cart if a person or object is detected in the travel path.
Rail-compatible battery carts — like the rail transport cart series from Xiigoo — offer higher maximum load capacities (up to 60,000 kg) but require permanent rail installation. Trackless models are preferred for multi-station layouts with frequent reconfiguration. Rail models suit fixed, high-throughput production lines with predictable material flow paths.
Hybrid facilities sometimes use trackless battery carts for slab yard transport and rail carts for in-line production feeding. The Natural Stone Institute notes that this combination is increasingly common in medium-to-high volume fabrication plants where layout flexibility and throughput speed are equally prioritized.
Battery Shuttle Car vs Other Slab Transport Options
To ensure the selection decision is informed, the table below compares battery shuttle cars with alternative transport methods used in stone fabrication.
| Criterion | Battery Shuttle Car | Forklift with Slab Clamp | Overhead Crane |
|---|---|---|---|
| Max typical load | 10,000–20,000 kg | 3,000–8,000 kg | 5,000–50,000 kg |
| Travel path flexibility | High (wireless remote) | High (vehicle-driven) | Fixed to bridge rail coverage |
| Single-operator feasibility | Yes (remote control) | Yes (driver-operated) | No (requires ground crew) |
| Operator training required | Low (basic remote training) | Moderate (forklift license) | High (certified crane operator) |
| Best suited for | Ground-level slab transfer between stations | Loading/unloading trucks and rack access | Heavy block lifting and machine feeding |
Summary of the Selection Checklist
When preparing to choose a battery shuttle car for a stone factory, the following checklist covers the essential decision points:
- Record the maximum slab weight and dimensions processed. Apply a 1.25× safety factor to determine required load capacity.
- Confirm that battery runtime exceeds the longest production shift by at least 30 minutes.
- Measure door widths, aisle clearances, and loading station heights to confirm the cart's overall dimensions fit the facility.
- Survey floor flatness across all travel paths to select appropriate wheel diameter and material.
- Decide between trackless and rail models based on whether the production layout is fixed or reconfigurable.
The XGM-BDC10T and XGM-BDC20T product pages provide full dimensional drawings and technical specifications that can be checked against facility measurements before purchase.
Frequently Asked Questions
A battery shuttle car and a battery transfer cart refer to the same type of equipment: a wireless, battery-powered platform vehicle for moving heavy materials. The term "shuttle car" is more common in North American stone fabrication, while "transfer cart" is used globally. There is no technical difference between the two terms.
Dv200 lead-acid batteries on industrial shuttle cars are rated for over 1,000 charge-discharge cycles. With one full cycle per day, the battery pack typically lasts 3 to 4 years. Proper charging discipline — avoiding deep discharges below 20% capacity — can extend service life to over 1,500 cycles.
Yes, provided the cart is equipped with sufficiently large wheels. Models with 630 mm diameter wheels handle floor irregularities up to ±5 mm over 3 meters. For severely uneven floors, concrete grinding or patching is recommended before deploying any powered transport vehicle to prevent structural stress on the cart frame.
Standard safety features include obstacle detection with automatic stop, audible alarm on activation, emergency stop button, and remote-controlled operation that keeps the operator at a safe distance. Trackless models additionally feature 60-degree in-situ rotation for maneuvering in tight spaces without manual load guiding.
No specialized certification is required beyond basic remote control operation training. Most operators can learn the control system in under 2 hours. Facilities with multiple carts should standardize on one control interface to minimize cross-training needs, following ANSI guidelines for industrial vehicle operator training programs.
Conclusion
Choosing the right battery shuttle car for a stone factory requires aligning equipment specifications with operational realities — load patterns, shift schedules, slab dimensions, and floor conditions. Key conclusions include: 1) Start with actual slab weight data, not estimates, and apply a safety margin. 2) Battery runtime of 8+ hours covers single shifts; double-shift operations need spare battery packs. 3) Table size must exceed the largest slab dimension by at least 100 mm on each side. 4) Wheel selection should follow a floor flatness survey rather than defaulting to the largest diameter. 5) Trackless models offer layout flexibility; rail models offer higher capacity. By systematically evaluating these five factors, fabrication facility managers can select a battery shuttle car that delivers reliable material transport without overcapacity or under-specification.